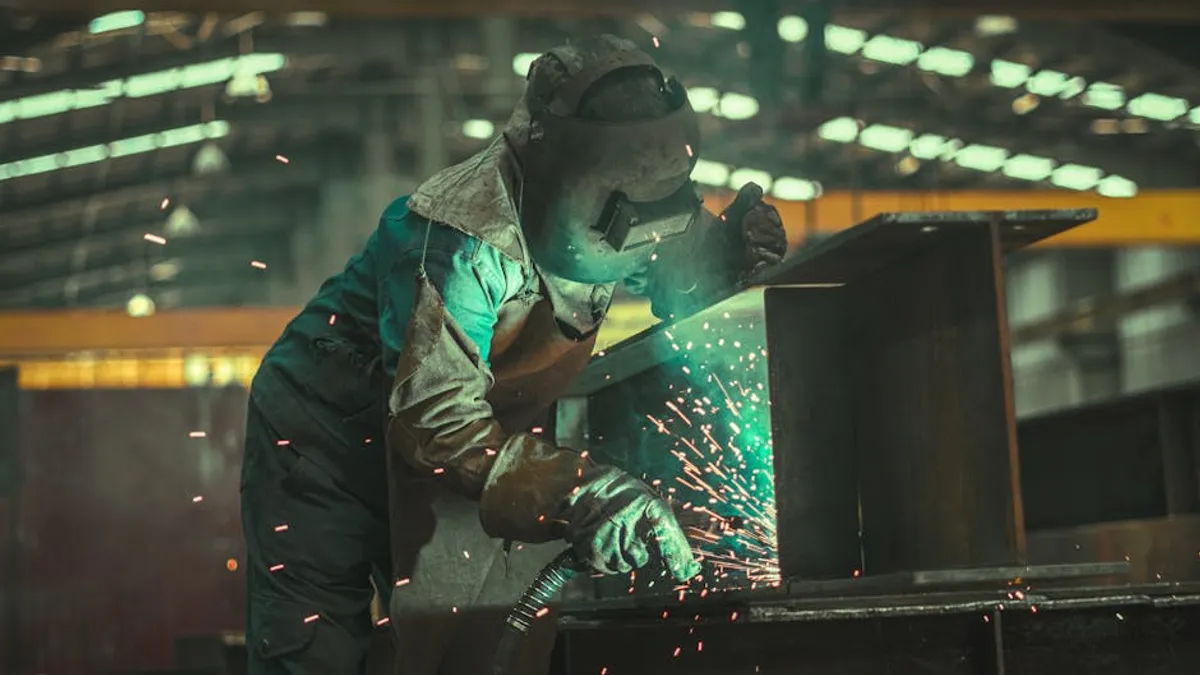
Achieving high-quality MIG welds consistently depends on numerous variables, with shielding gas pressure standing as a critical, yet often overlooked, factor. Incorrect gas pressure directly impacts arc stability, weld penetration, and final weld appearance, leading to costly defects like porosity, excessive spatter, and poor fusion. Understanding and precisely controlling this parameter is not merely about adherence to specifications; it’s about optimizing material utilization, reducing rework, and ensuring structural integrity. This guide details the essential settings and practical troubleshooting steps to maintain optimal gas flow for efficient and reliable MIG welding operations.
Understanding Shielding Gas and Its Role
Shielding gas serves a fundamental purpose in MIG welding: protecting the molten weld pool and the arc from atmospheric contamination. Oxygen and nitrogen from the air react with the hot metal, causing porosity, brittleness, and reduced corrosion resistance. The shielding gas creates an inert or semi-inert envelope around the arc and weld pool, preventing these detrimental reactions. The type of gas selected influences arc characteristics, penetration profile, and the mechanical properties of the weld metal.
Common Shielding Gases for MIG
The choice of shielding gas is dictated by the base metal, material thickness, and desired weld properties. Each gas or mixture offers distinct advantages:
- 100% Argon (Ar): Primarily used for welding non-ferrous metals like aluminum, magnesium, copper, and reactive metals. Argon provides a stable arc, good penetration, and clean welds. Its higher density helps it shield effectively, but it can produce a narrow, finger-like penetration profile on steel.
- 100% Carbon Dioxide (CO2): A reactive gas, CO2 is the least expensive option and provides good penetration for steel. It generates a hotter arc, leading to more spatter and a harsher arc compared to argon-rich mixtures. It's often favored for thicker materials and in applications where spatter cleanup is tolerable.
- Argon/CO2 Mixes: The most common choice for welding carbon and low-alloy steels.
- 75% Ar / 25% CO2 (C25): An industry standard for short-circuit MIG welding on steel, offering a stable arc, good bead appearance, and reduced spatter compared to 100% CO2. It supports all transfer modes.
- 90% Ar / 10% CO2 (C10): Preferred for spray transfer welding on steel, delivering higher deposition rates, deeper penetration, and minimal spatter.
- Argon/Oxygen Mixes: Typically used for spray transfer on stainless steels and some carbon steels. Small additions of oxygen (1-5%) stabilize the arc, improve bead wetting, and enhance penetration. However, higher oxygen content can lead to oxidation and embrittlement.
- Argon/Helium Mixes: Helium increases arc voltage and heat input, making it suitable for welding thick aluminum, copper, and stainless steel. It improves penetration and travel speed but is significantly more expensive and requires higher flow rates due to its lighter density.
Optimal Gas Pressure Settings
The term "gas pressure" in welding often refers to the flow rate, measured in cubic feet per hour (CFH) or liters per minute (L/min), rather than the pressure within the cylinder (PSI). A flowmeter, not just a pressure gauge, is essential for accurate measurement and control of shielding gas delivery to the torch nozzle.
Factors Influencing Flow Rate
Establishing the correct flow rate is not a fixed parameter; it adapts to several operational variables:
- Wire Diameter and Material Thickness: Thicker materials and larger wire diameters generally require higher flow rates to adequately shield the larger weld pool.
- Welding Process (Transfer Mode): Short-circuit transfer typically uses lower flow rates (e.g., 15-25 CFH) compared to spray or pulsed spray transfer (e.g., 30-50+ CFH), which involve larger, hotter weld pools.
- Nozzle Size: Larger nozzles can require slightly higher flow rates to maintain effective coverage, though excessive flow through any nozzle size can cause turbulence.
- Joint Type and Welding Position: Complex joint geometries or out-of-position welding might necessitate adjustments to ensure complete coverage.
- Environmental Conditions: Drafts, fans, or open bay doors in the welding area can disrupt the gas shield, requiring increased flow rates to compensate. This is a common but often overlooked cause of porosity.
General Flow Rate Guidelines
While specific settings will vary by machine and application, a practical starting point for most MIG welding operations on steel with an Ar/CO2 mix is 20-30 CFH. For aluminum, especially with 100% Argon, flow rates can range from 20-40 CFH depending on thickness and wire diameter. It is crucial to consult the welding machine manufacturer's recommendations and conduct test welds to fine-tune settings for optimal results. A good flowmeter will have a ball float indicator that provides a direct reading of CFH, allowing for precise adjustment.
Pro Tip: Always verify your gas flow rate using a flowmeter at the torch nozzle, not just at the regulator. Restrictions in the gas line or torch can significantly reduce the actual flow reaching the weld pool, even if the regulator indicates the correct setting. A simple flow checker held against the nozzle provides the most accurate reading of gas delivery.
Identifying and Troubleshooting Gas Pressure Issues
Deviations from optimal gas flow manifest in distinct weld defects, signaling a need for immediate troubleshooting.
Symptoms of Low Gas Flow
Insufficient shielding gas is a primary cause of weld quality issues:
- Porosity: The most common symptom. Small holes or voids appear in the weld bead, indicating atmospheric gases have contaminated the molten metal. This significantly weakens the weld.
- Excessive Spatter: While several factors cause spatter, inadequate shielding can lead to an unstable arc that throws off more molten metal.
- Unstable Arc: The arc may flicker, wander, or extinguish frequently, making welding difficult and inconsistent.
- Contaminated Welds: Discoloration, particularly a black or sooty appearance on the weld or surrounding material (especially noticeable on stainless steel or aluminum), indicates oxidation.
Symptoms of High Gas Flow
While less common than low flow, excessive gas flow also presents problems:
- Turbulence at the Nozzle: High flow rates can create a turbulent gas stream that pulls ambient air into the shielding gas envelope, defeating its purpose and leading to porosity.
- Increased Gas Consumption: Wasted gas directly translates to higher operating costs. Over-setting the flow rate by even a small amount can significantly deplete cylinders faster than necessary.
- Cooling Effect: Extremely high flow can cool the weld pool, potentially affecting penetration and bead profile, though this is less common than turbulence issues.
Common Troubleshooting Steps
When weld quality issues arise, systematically check these components:
- Gas Cylinder Level: Ensure the cylinder is not empty or critically low. A pressure gauge on the regulator will indicate cylinder pressure.
- Regulator and Flowmeter: Inspect for damage, leaks, or blockages. Confirm the flowmeter's ball is freely moving and indicating the set CFH.
- Hose Connections: Tighten all connections from the cylinder to the welding machine and to the torch. Use leak detection spray (soapy water) to identify pinhole leaks in hoses or fittings.
- Torch Components: Check the gas diffuser, contact tip, and nozzle for spatter buildup or damage. A clogged diffuser restricts gas flow, while a damaged nozzle can disrupt the gas stream. Clean or replace as needed.
- Welding Environment: Eliminate drafts caused by fans, open doors, or HVAC systems. Consider using welding screens to create a more controlled environment.
- Nozzle-to-Work Distance (Stick Out): Maintain a consistent stick out. An excessively long stick out increases the distance the shielding gas must travel, making it more susceptible to disruption.
Ensuring Consistent Weld Quality
Mastering MIG welding gas pressure is an ongoing process of observation, adjustment, and verification. While general guidelines provide a starting point, the optimal settings are often specific to the exact welding setup, materials, and environmental conditions. Regular inspection of equipment, proactive troubleshooting, and a keen eye for weld defects are essential practices. By prioritizing precise gas flow management, operators can significantly enhance weld quality, reduce material waste, and improve overall operational efficiency, directly contributing to more reliable and cost-effective fabrication.
Frequently Asked Questions
How do I measure MIG welding gas flow rate?
Gas flow rate is measured using a flowmeter, typically integrated into the regulator or as a separate inline device. The most accurate method involves using a handheld flow checker directly at the torch nozzle to confirm the gas volume exiting the torch.
What are the primary indicators of insufficient shielding gas?
The most common indicators are porosity (small holes in the weld), excessive spatter, an unstable arc, and discoloration or black soot on the weld bead, especially noticeable on stainless steel or aluminum.
Can too much shielding gas cause welding problems?
Yes, excessive gas flow can create turbulence at the nozzle, drawing atmospheric air into the gas shield and leading to porosity. It also results in significant gas waste, increasing operational costs unnecessarily.
How often should I check my gas flow settings?
It is best practice to check your gas flow settings at the beginning of each welding session and whenever you change welding parameters, materials, or experience any weld quality issues. Regular visual inspection of the flowmeter is also recommended during welding.